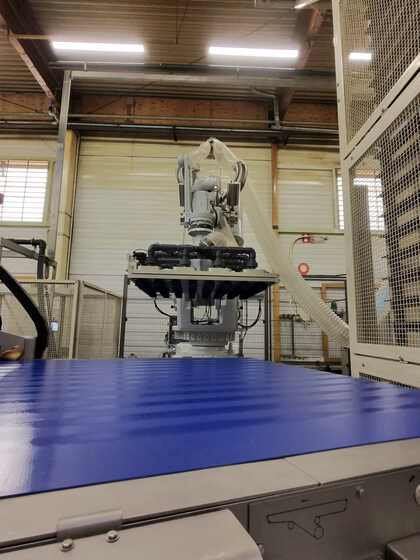
Demoulding a hot, porous and greasy product without marking it is the sticking point of bakery lines. A conventional suction cup fails by nature: the open crumb lets the vacuum leak away, and compensating by increasing the vacuum means crushing the product. For a madeleine production line in France, TECH3D designed a robotic cell that reverses the usual logic: regulating an airflow rather than a vacuum level, and demoulding an entire tray in a single cycle.
🌬️ Our solution: regulate a flow, not a vacuum
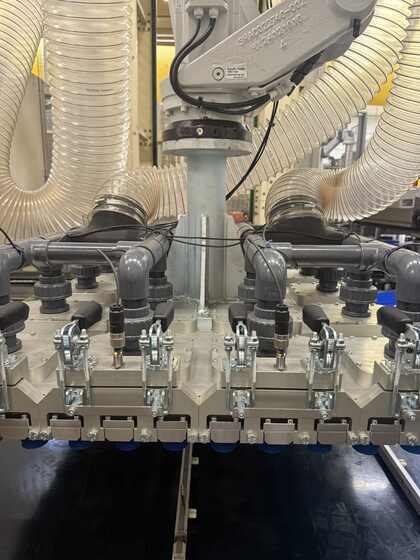
Ejectors on the market regulate a high vacuum at low flow: perfect on a sealed surface, they are defeated by a porous crumb. Our cell uses a high-flow turbine with frequency control, which continuously compensates for the leak at a vacuum low enough not to mark the product. The leak is accepted rather than fought: this change of principle is what makes demoulding possible without crushing the part.
Twelve gripping bars, fitted with bellows suction cups in detectable food-grade silicone, are controlled in groups of three. Only the areas actually filled are activated, which keeps the vacuum where it is useful and allows the grip to be adapted to the tray format without changing tools. A vacuum switch on each bar checks the grip; the detection threshold was determined through successive tests on real product, because a circuit that leaks continuously, and whose leak drifts as grease builds up, cannot be set from a catalogue.
📋 Technical specifications
| Gripping capacity | 96 pieces per cycle (12 bars × 8) | Manipulator | ABB articulated robot |
| Throughput | 2 to 9 trays per minute | PLC | Siemens S7-1200 |
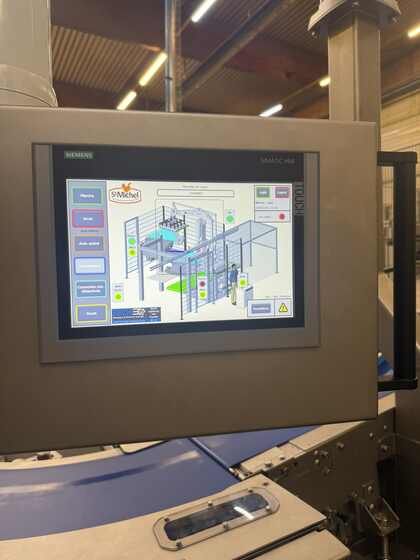
| Success rate | ≥ 98% | Supervision | SIMATIC panel, recipe-based operation |
| Gripping principle | High-flow, low-vacuum suction | Remote maintenance | Ewon industrial router |
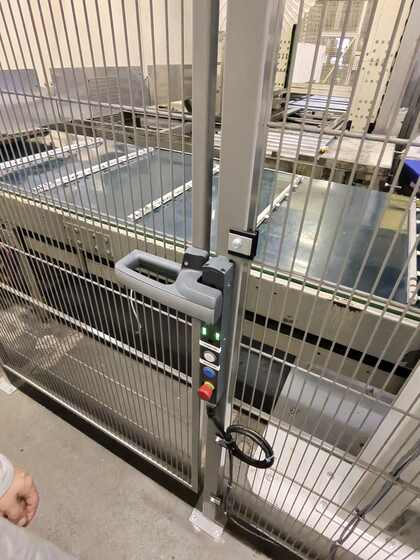
| Gripping elements | Bellows suction cups, detectable food-grade silicone | Safety | Fenced cell, interlocked doors, emergency stops |
| Zoning | Bars controlled in groups of three | Integration | Connection to the existing line supervision |
| Vacuum generation | Frequency-controlled turbine | Target products | Madeleines, sponge cakes, soft products demoulded hot |
| Grip check | Vacuum switch, per bar | Placing | Synchronised active blow-off |
🎯 What makes the difference
Grip checking despite the leak
On a circuit that leaks continuously and whose leak drifts as grease builds up, a standard vacuum switch can no longer tell anything apart. The detection threshold used for this cell was determined through successive tests on real product, not by theoretical setting.
One format, one recipe
Path, active bars, vacuum and throughput are stored per recipe from the SIMATIC panel. Changing product runs is a simple selection, with no mechanical intervention on the cell.
🛠️ The TECH3D skills involved in this project
This cell illustrates the full range of know-how we put at the service of our industrial customers, from study to commissioning:
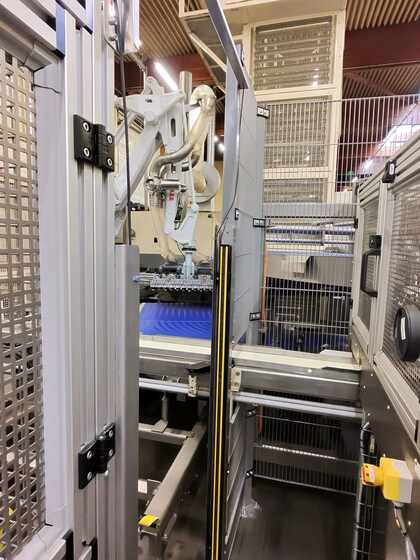
Robotics: integration of an ABB articulated robot for handling and for synchronising placement with the downstream packaging machines.
Automation: programming of a Siemens S7-1200 PLC and a supervision system on a SIMATIC panel, with recipe-based operation for product changes without mechanical intervention.
Pneumatic and industrial vacuum engineering: custom design of a gripping system based on regulated airflow rather than conventional vacuum: frequency-controlled turbine, bars zoned in groups of three, and grip-check calibration through tests on real product.
Machine safety: design of a fenced cell with interlocked doors and emergency stops, compliant with the requirements of food production lines.
Remote maintenance: integration of an Ewon industrial router for remote monitoring and support of the cell.
System integration: connection of the cell to the customer’s existing line supervision, without interrupting the production flow.
As with all our projects, the study, design, build and commissioning were carried out in-house by our teams, using our own technology building blocks.
📈 Results in production
The cell is in operation on an industrial madeleine line in France, with a demoulding success rate of 98% or more, a throughput of 2 to 9 trays per minute and a gripping capacity of 96 pieces per cycle – a complete tray demoulded and placed on every pass of the robot.
🔄 A transferable solution
The regulated-flow gripping principle is not limited to madeleines: it can be applied to any porous or fragile product demoulded hot – sponge cakes, soft biscuits and, more broadly, any food product for which a conventional suction cup marks or crushes the piece. Each cell is still custom-designed, based on our technology building blocks and the specific constraints of each line.
🧩 Why choose TECH3D for your project?
Since 2010, TECH3D has supported manufacturers in their robotisation and automation projects from its base in the Grand Est region of France, close to Strasbourg, Metz and Nancy. We approach every special gripping project with the same method: analysis of the product and the constraint, custom design, then deployment and follow-up via remote maintenance.
Facing a difficult gripping or demoulding problem on your line? Contact our team for an analysis of your product and a recommendation tailored to your process.